PlantPulse — Manufacturing Intelligence, Delivered
Home · PerformIQ
PerformIQ · AI performance intelligenceAvailable

The intelligence at the centre of your plant

PerformIQ controls, optimises, improves and learns across quality, OEE, process, energy, raw-material risk, maintenance and standards. Every signal becomes an owned decision, every decision is verified, and what works becomes the standard.

Four loops, one engine

Control · Optimise · Improve · Learn

Control

What needs a response now?

Live shift control, due checks, deviations with approved responses, quality from incoming to dispatch, breakdowns and restart checks.

Optimise

Which feasible option is better?

OEE and losses ranked by impact, plan vs actuals, flow and constraints, energy per unit against baseline.

Improve

What stops the loss returning?

Chronic problems and root cause, kaizen with benefits tracking, maintenance risk and inspection.

Learn

Which standard should change?

Verified results become proposed changes to limits, operating windows and responses, approved and versioned.

Control · Role Homes and My Work

Every role starts the shift knowing what needs them

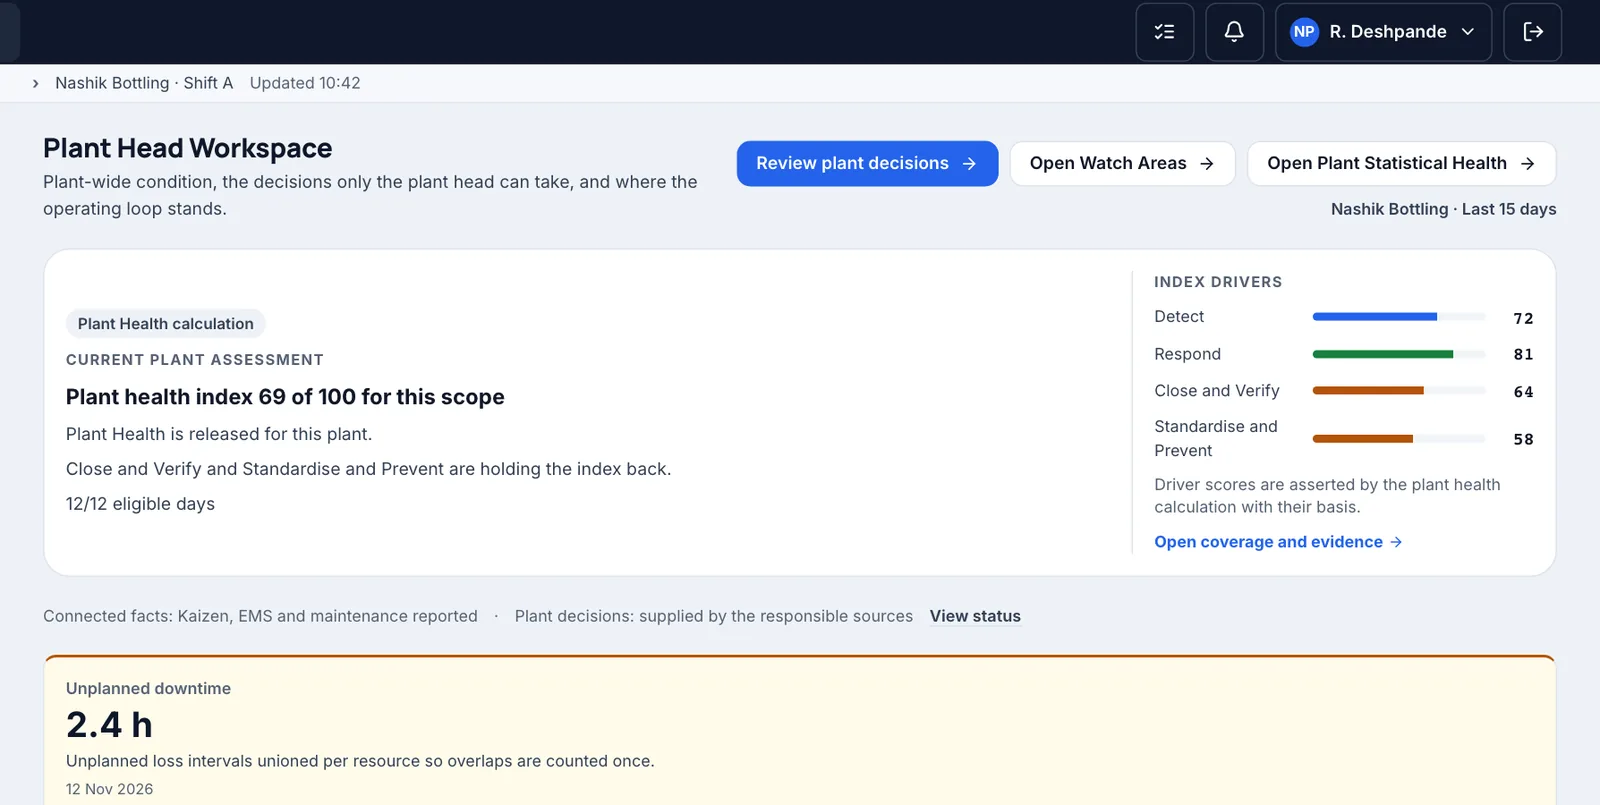
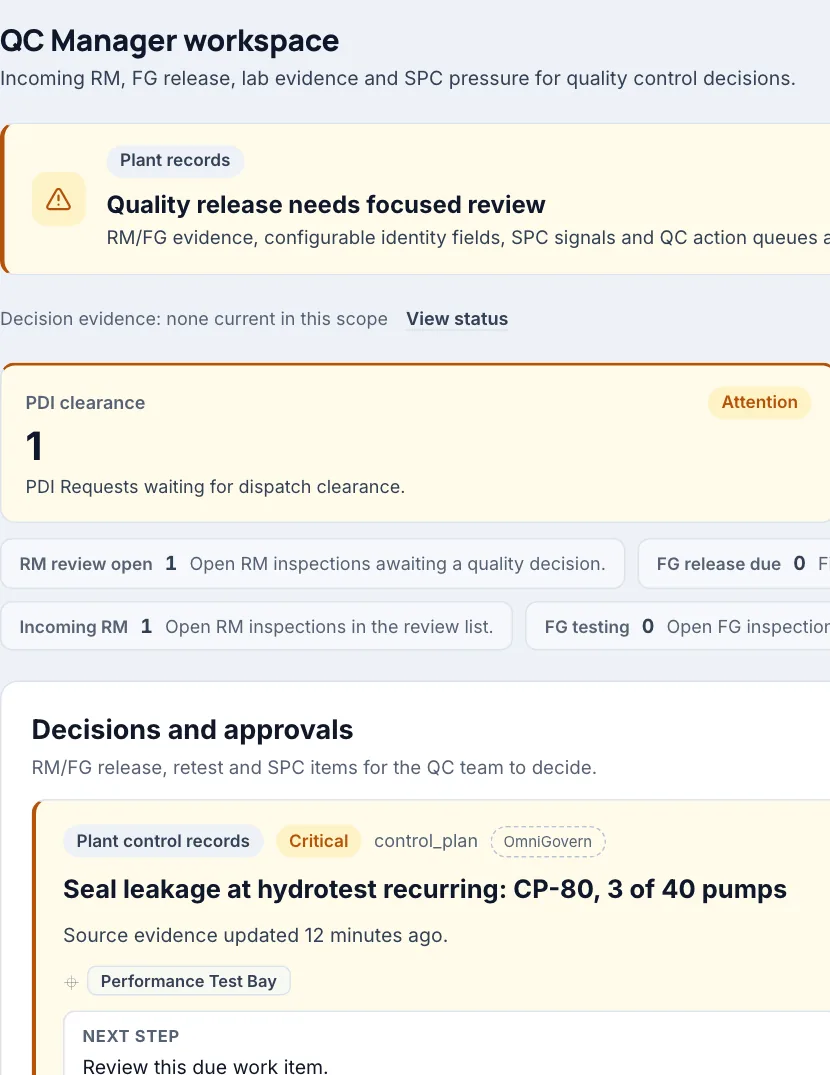
Each manager has a decision home: plant condition, the decisions waiting with their evidence, and key figures. Personal tasks sit in My Work. Nobody compiles a morning report.

Plant Head home · Sunvale Beverages, Nashik Bottling (fictional)
QC Manager home · Arvenko Engineering, Pune Pump Assembly (fictional)
  • Plant Health Index and key figures, calculated not compiled
  • Decision cards with evidence and a recommended next step
  • Same layout for every role; only decisions and permissions differ
Control · Live shift control

The shift runs from the floor, online or offline

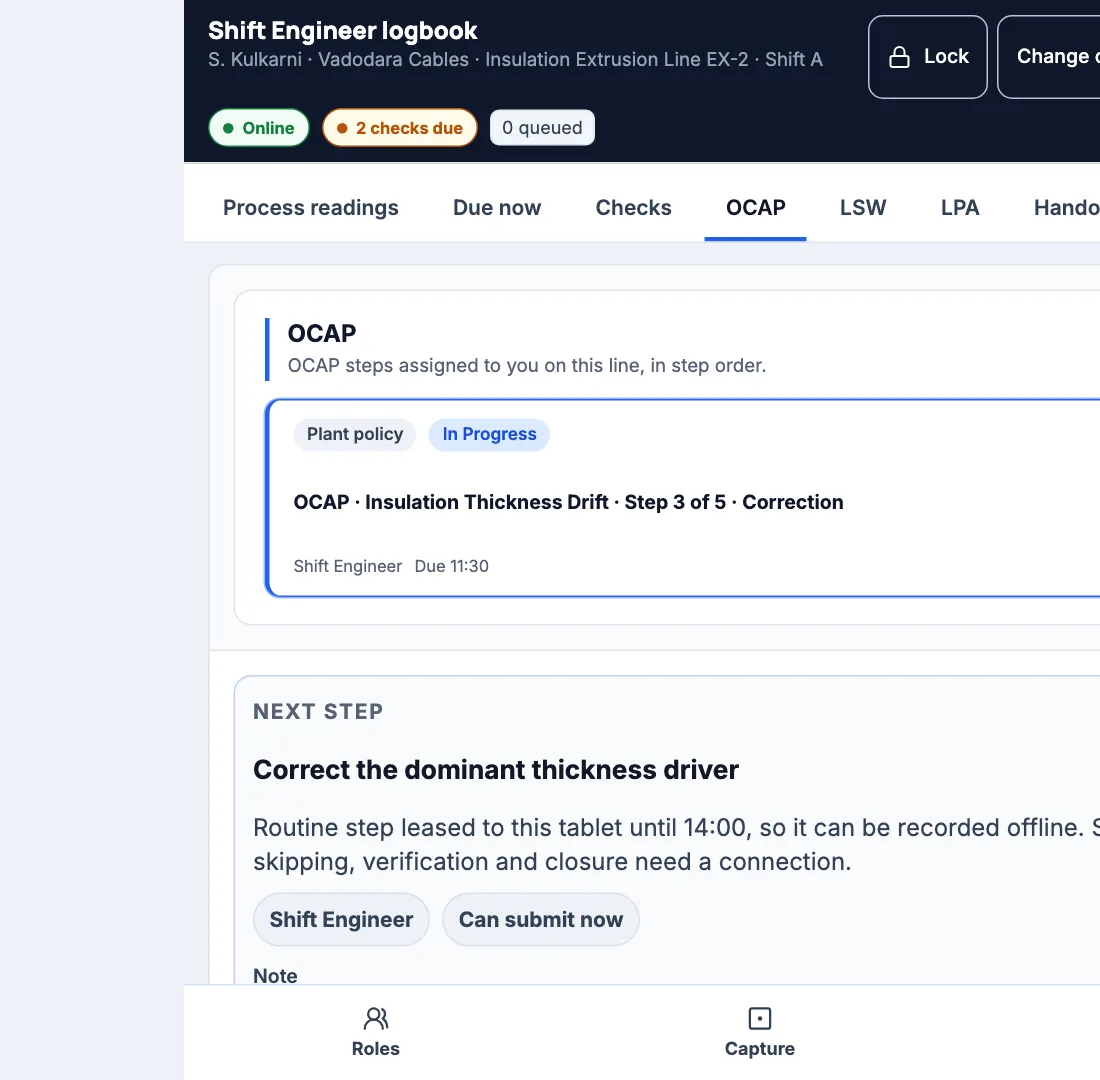
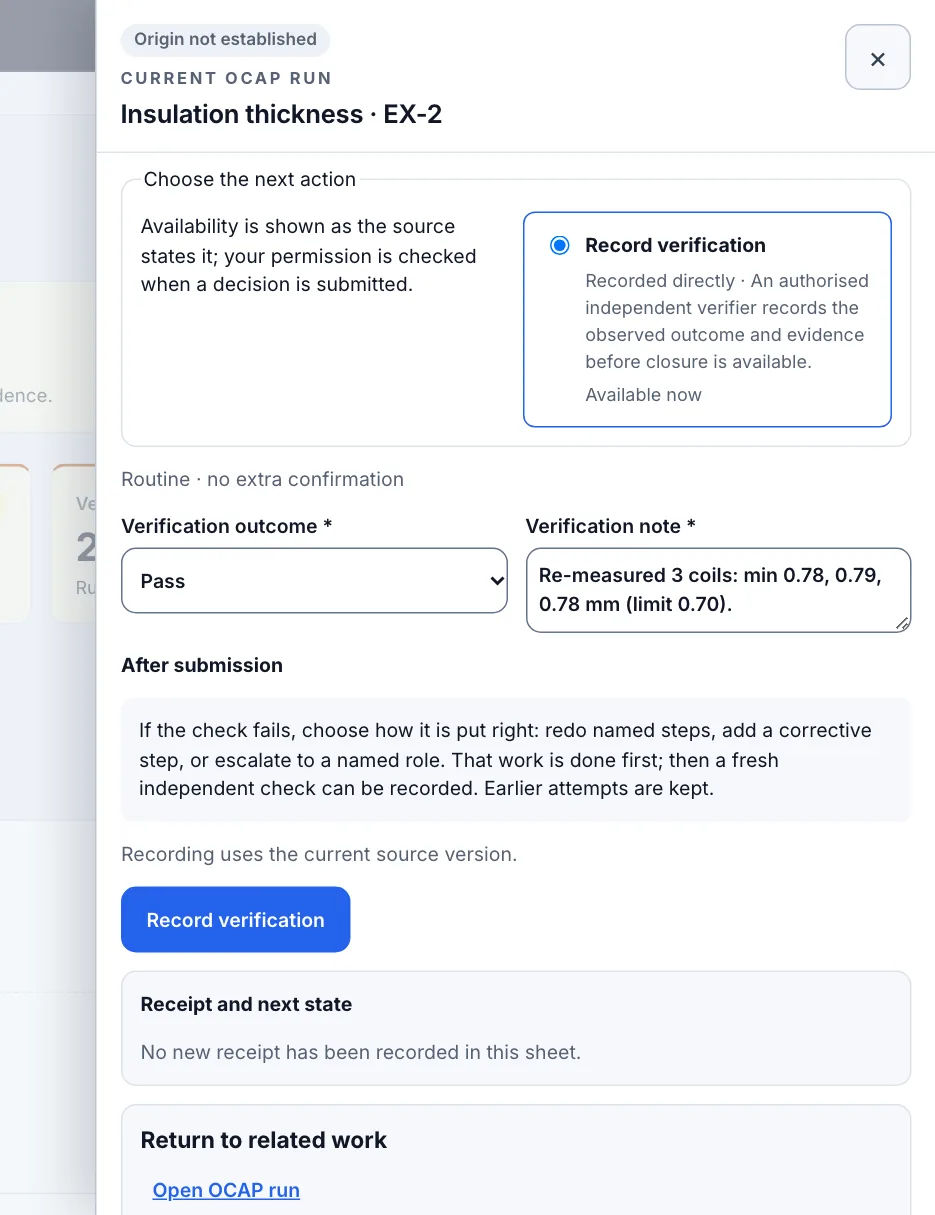
Due checks and response steps reach the right person on shared tablets with personal sign-in. A deviation brings its approved response, and a different person verifies the result before anything closes.

Response step on a shared tablet · Meridia Cables, Vadodara (fictional)
Independent verification of a response run (fictional)
  • Approved response plans executed step by step
  • Routine steps recorded offline and synced later
  • Closure only after independent verification
Control · Quality from incoming to dispatch

Quality decisions reach the person with authority to decide

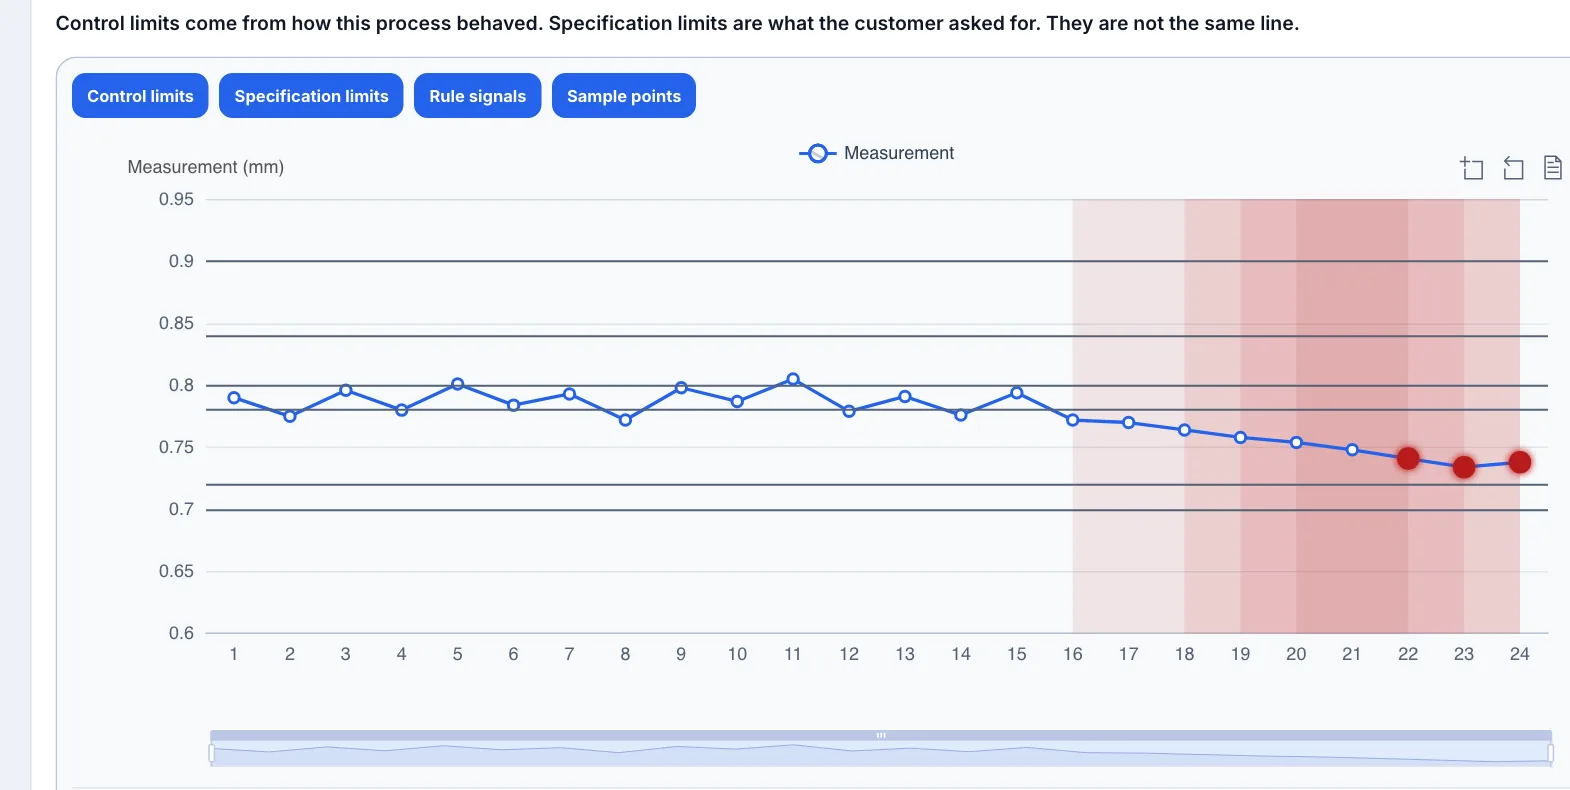
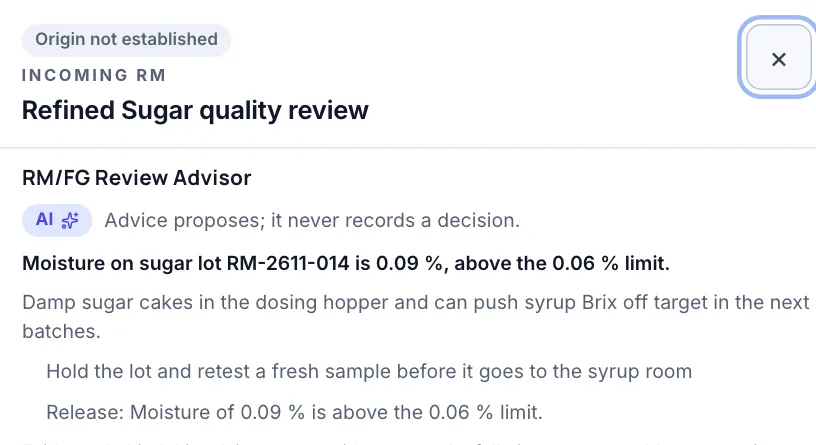
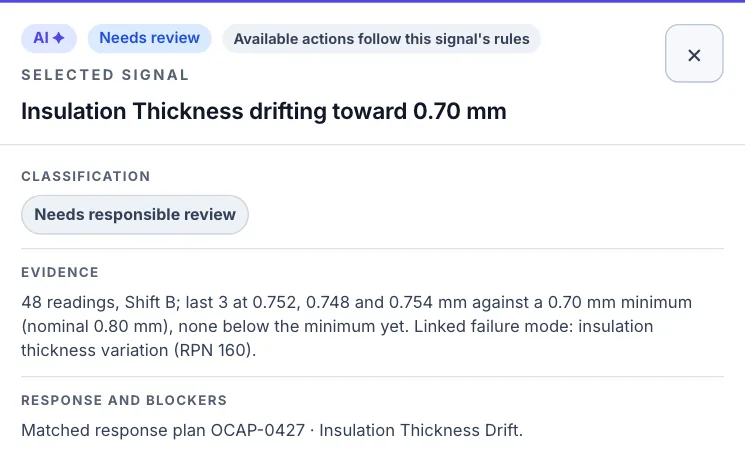
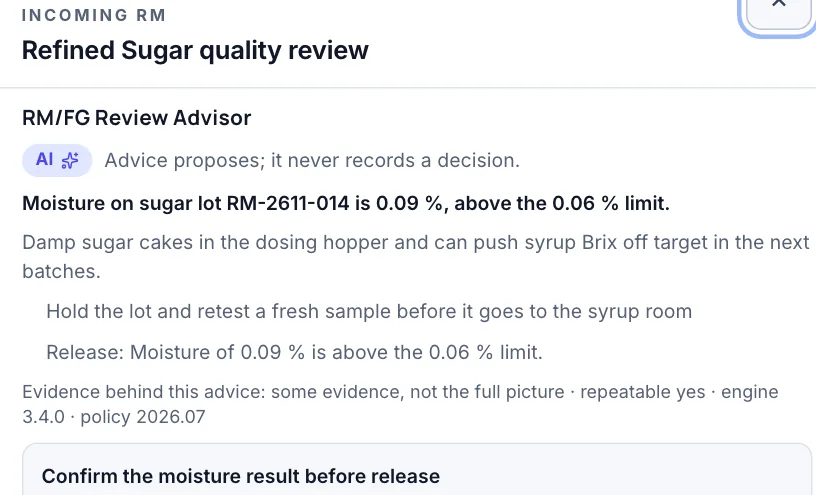
Incoming lots, in-process drift and finished goods each go to the right decision-maker. AI advice sits beside the decision but never makes it. Dispatch needs pre-dispatch inspection and clearance by two different people.

SPC: insulation thickness drifting toward its minimum (fictional)
Incoming sugar lot held over its moisture limit, with AI advice (fictional)
  • Drift caught before it becomes scrap, explained in plain words
  • Lots held automatically, released by the authorised role
  • Certificates generated from the release decision itself
Control · Production and materials

An operational record from raw material in to finished goods out

Plan release, material issue and measured consumption, WIP and genealogy, output, finished goods and dispatch release are recorded as people work, as completely as a good ERP on the shop floor, without transaction keying.

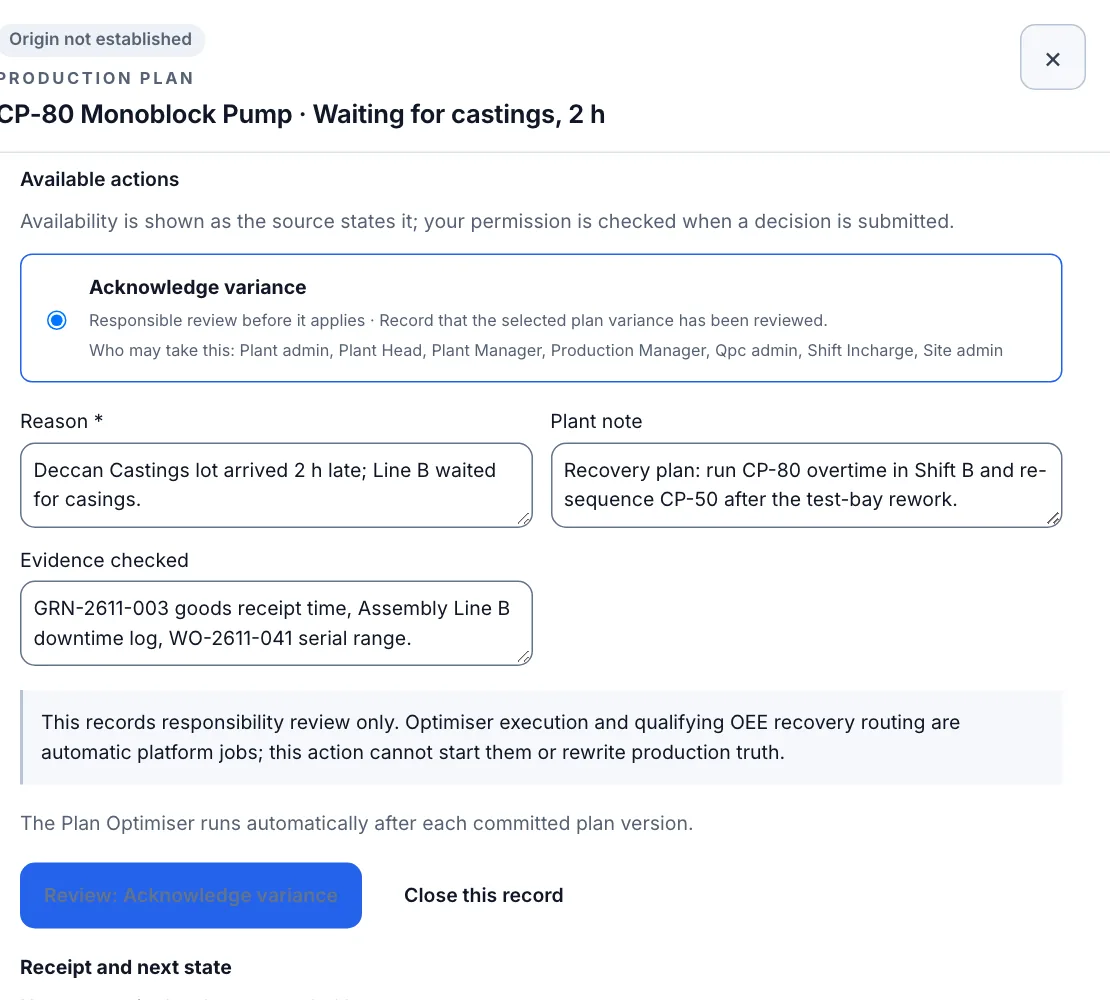
  • Variances against the released plan become owned decisions, with a reason
  • Reconciliation closes itself within tolerance and raises a decision when it does not
  • Lot trace backward and forward; confirmations go back to your ERP
Plan variance decision with reason, fictional pump plant
Variance decision with reason · Pune Pump Assembly (fictional)
Optimise · Process Intelligence · rare in plant software

See where your flow really breaks

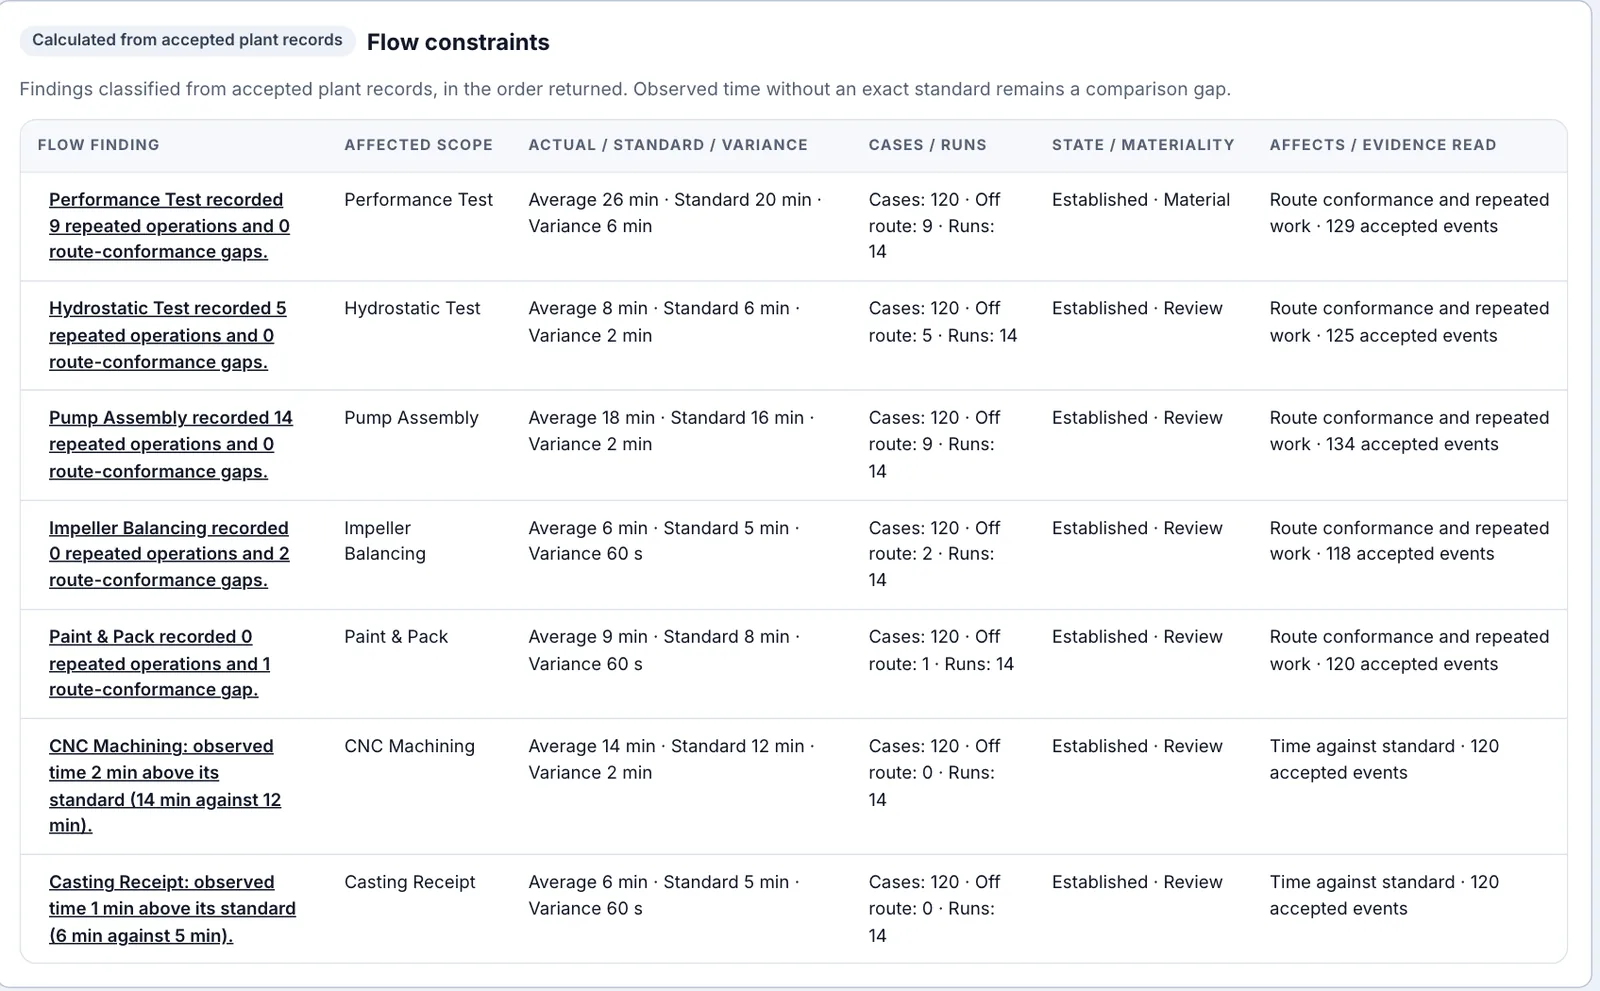
Process Intelligence compares how every unit actually moved with the certified route and standard times, from records the plant already keeps. It finds the real constraint and the route deviations, and explains them, without a separate process-mining project.

Process Intelligence flow constraints and route deviations, fictional pump plant
Flow constraints and route deviations · Pune Pump Assembly (fictional)
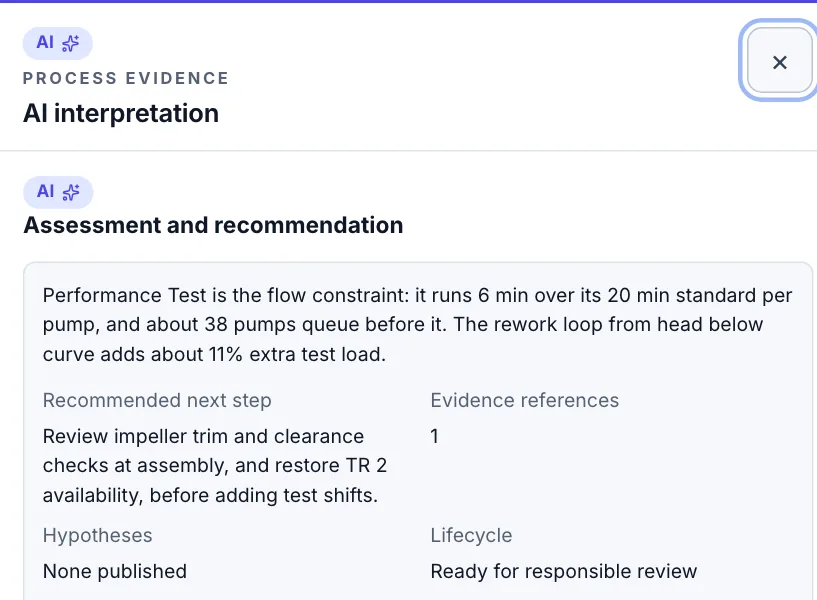
AI interpretation of the flow constraint
AI interpretation of the constraint

Actual route vs certified route

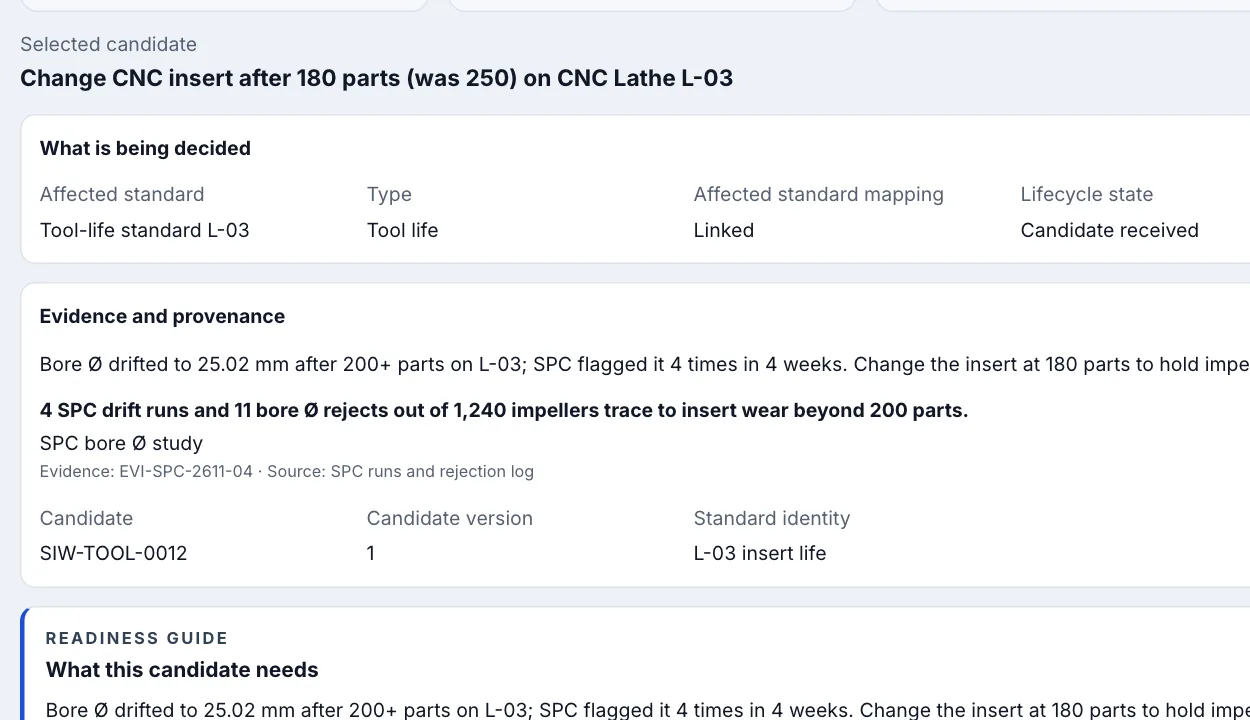
Rework loops from test back to assembly, repeated hydrotests after seal leaks, skipped balancing and out-of-order steps, found automatically.

The constraint, explained

Performance test runs 26 min per pump against a 20 min standard, with about 38 pumps queued. The page shows why.

What to fix first

AI recommends the next step, for example impeller trim checks and test-rig availability before adding shifts. The Production Manager decides.

Optimise · Performance and energy

See where performance is really lost, and what it costs

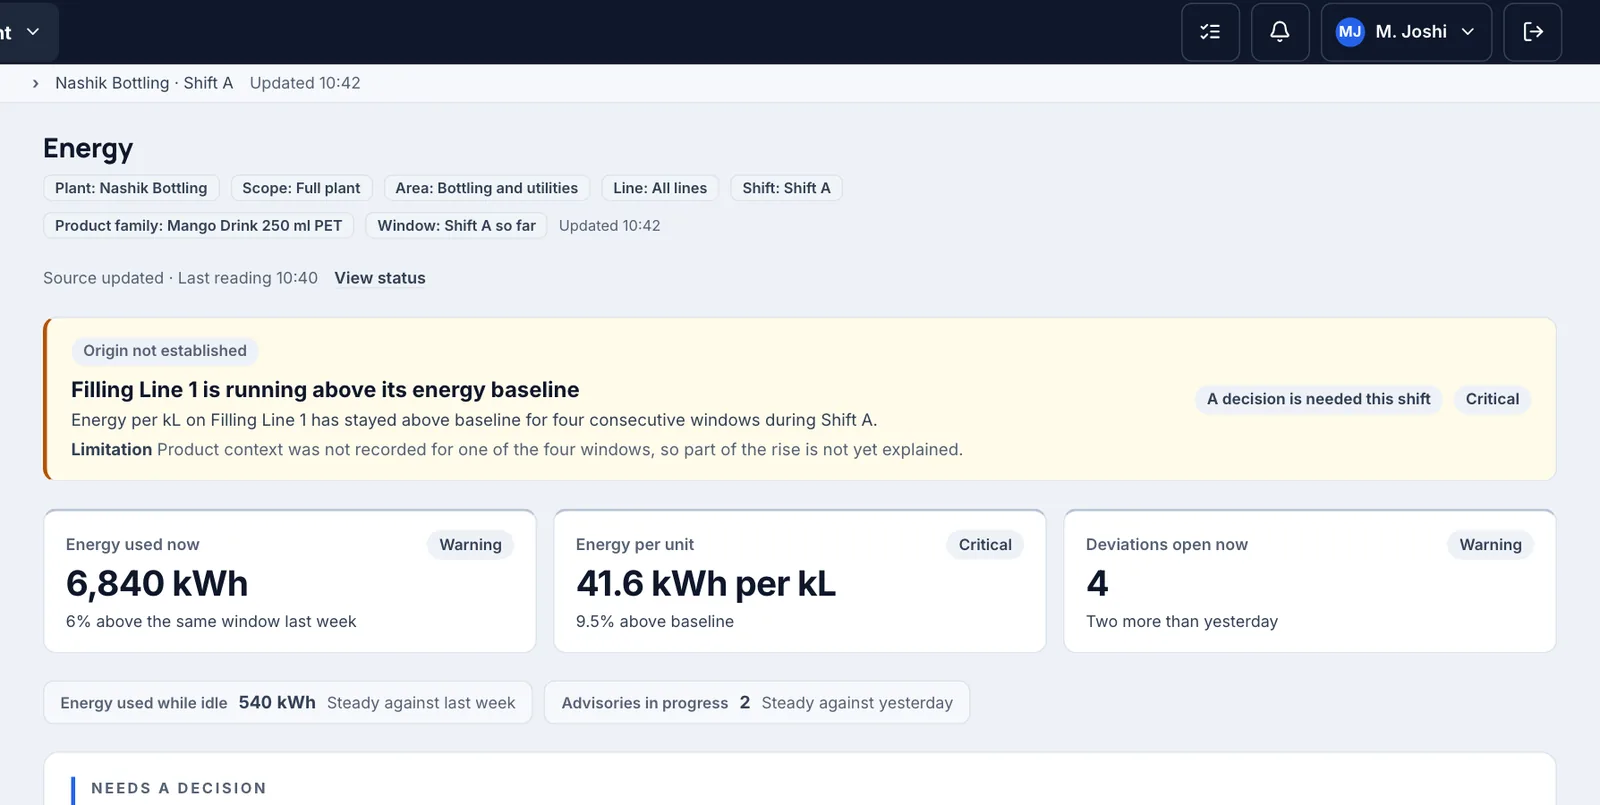
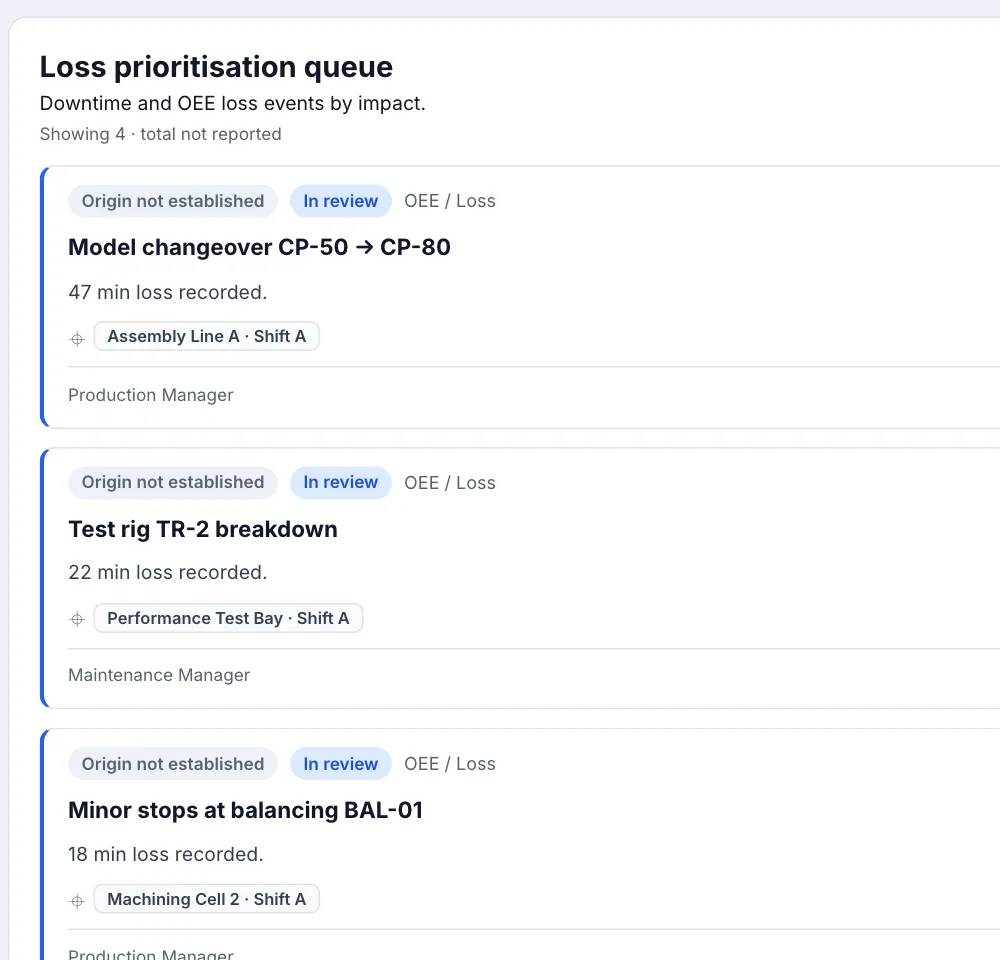
OEE and losses are calculated with one definition per KPI across lines and plants, ranked by impact, each with an owner. Energy per unit is tracked against its baseline and linked to the likely cause.

Energy per kL against baseline · Nashik Bottling (fictional)
OEE losses ranked by impact · Pune Pump Assembly (fictional)
  • Changeovers, breakdowns and minor stops ranked biggest first
  • One owner per loss, acknowledged with a reason
  • Energy savings counted only from verified periods
Improve and Learn

Improvement that pays, and learning that sticks

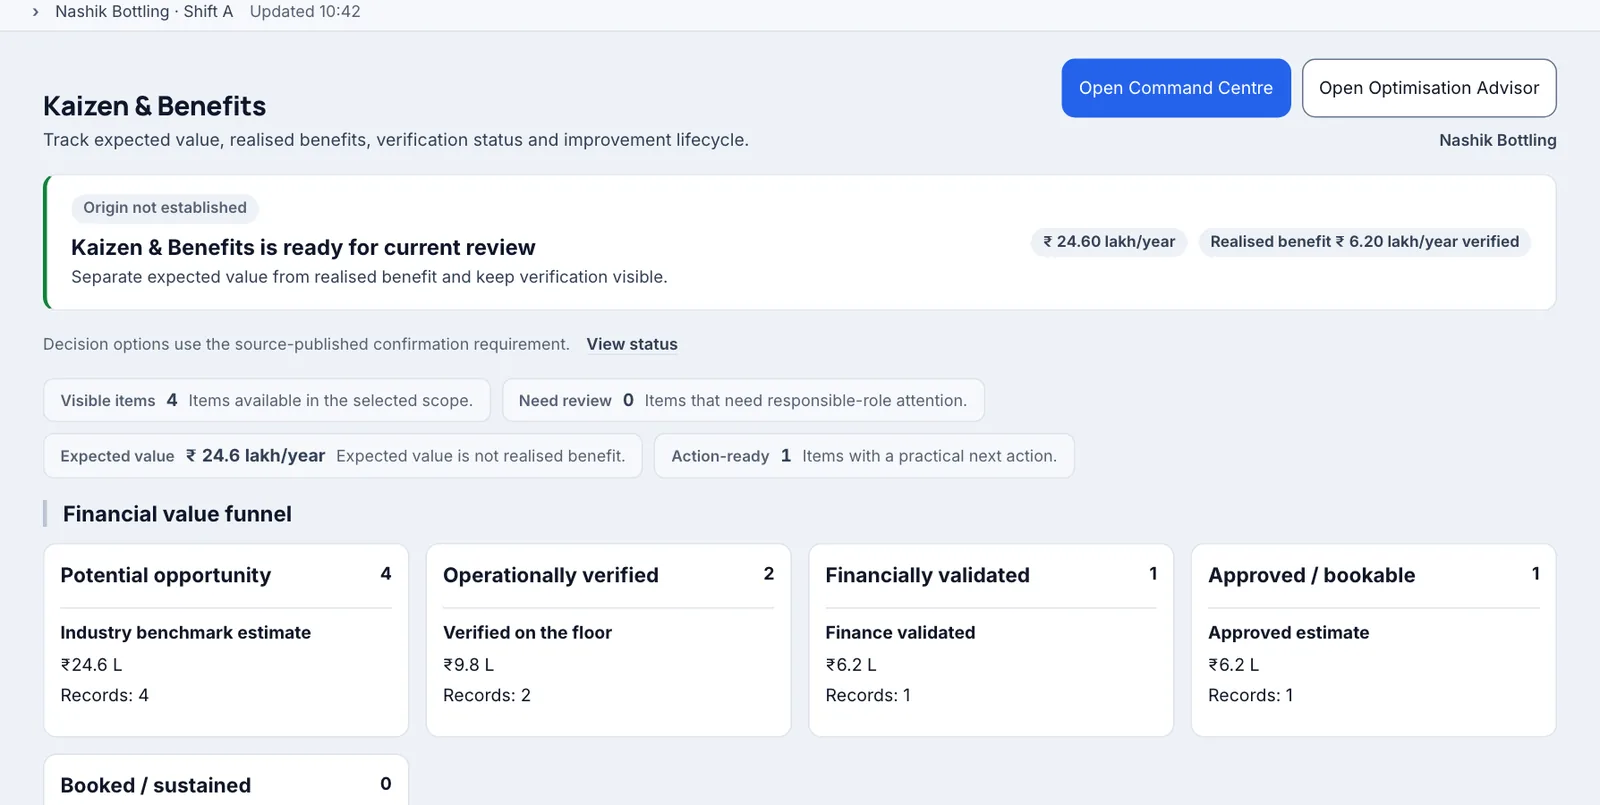
Kaizen benefits are kept honest on a value ladder: expected, implemented and accepted savings, in rupees, kept apart. A verified improvement proposes the change to the standard, so the next run starts better.

Kaizen & benefits value ladder · Nashik Bottling (fictional)
Proposed standard change from verified learning · Pune Pump Assembly (fictional)
  • Every figure shows the basis it was calculated on
  • Standard changes go through your approval and keep their history
  • Chronic problems and root-cause cases tested against evidence
PlantPulse AI in PerformIQ

4 AI assistants, built into the work

PlantPulse is a Manufacturing AIOS: AI is part of the operating loop, not a chatbot on the side. It senses the plant, interprets what is happening, recommends the next step, and hands the decision to the accountable role. The result is verified, and what works becomes the standard.

  1. Sense
  2. Interpret
  3. Recommend
  4. Govern
  5. Execute
  6. Verify
  7. Learn
Control Assistant in PlantPulse, fictional demo data
PlantPulse AI · PerformIQAvailable

Control Assistant

What needs a response now, and which approved response fits?

  • Explains the live signal with its evidence and limits
  • Matches the approved response plan for that signal
  • Watches due checks, missed checks and response SLAs
  • Escalates to the next role when a decision waits too long
Example: Insulation thickness drifting toward 0.70 mm on extrusion line EX-2
Evidence and its strength shownDecides: Shift InchargeNo direct plant change
Quality & Statistics Advisor in PlantPulse, fictional demo data
PlantPulse AI · PerformIQAvailable

Quality & Statistics Advisor

Is the process statistically sound, and what does quality need first?

  • Reads SPC rules, capability, stability and drift continuously
  • Recommends accept, retest, hold or escalate on incoming and finished lots
  • Says what quality needs first: containment before improvement
  • Links process drivers to quality outcomes with stated strength
Example: Sugar lot over its 0.06 % moisture limit, held at incoming
Evidence and its strength shownDecides: QC ManagerNo direct plant change
Optimisation & Kaizen Advisor in PlantPulse, fictional demo data
PlantPulse AI · PerformIQAvailable

Optimisation & Kaizen Advisor

Which improvement is better, what would it change, and what should we improve next?

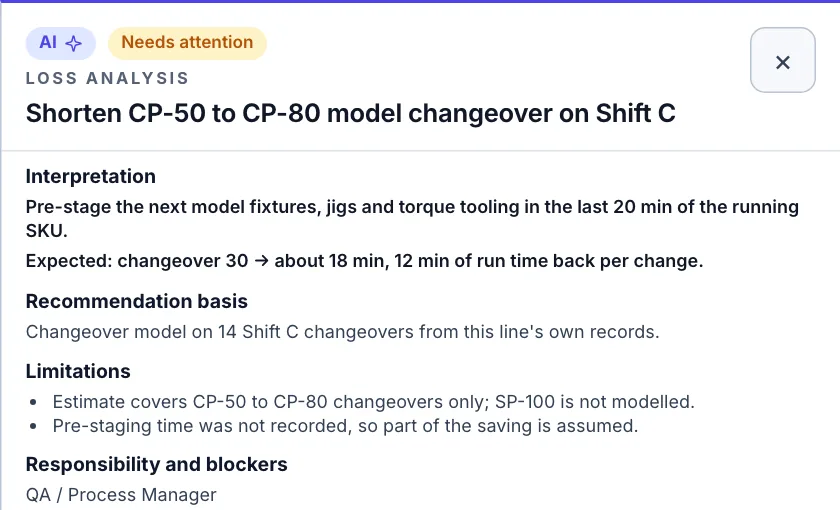
  • Ranks options across plan, process windows, OEE losses, material risk, maintenance and energy
  • States what each option would change and who owns it
  • Ranks kaizen opportunities and tracks benefits on a value ladder
  • Proposes better operating windows from verified results
Example: Pre-stage fixtures to cut a CP-50 → CP-80 changeover from 30 to 18 min
Evidence and its strength shownDecides: Production ManagerNo direct plant change
Energy Assistant in PlantPulse, fictional demo data
PlantPulse AI · PerformIQAvailable

Energy Assistant

Where is energy drifting from its baseline, and what is it linked to?

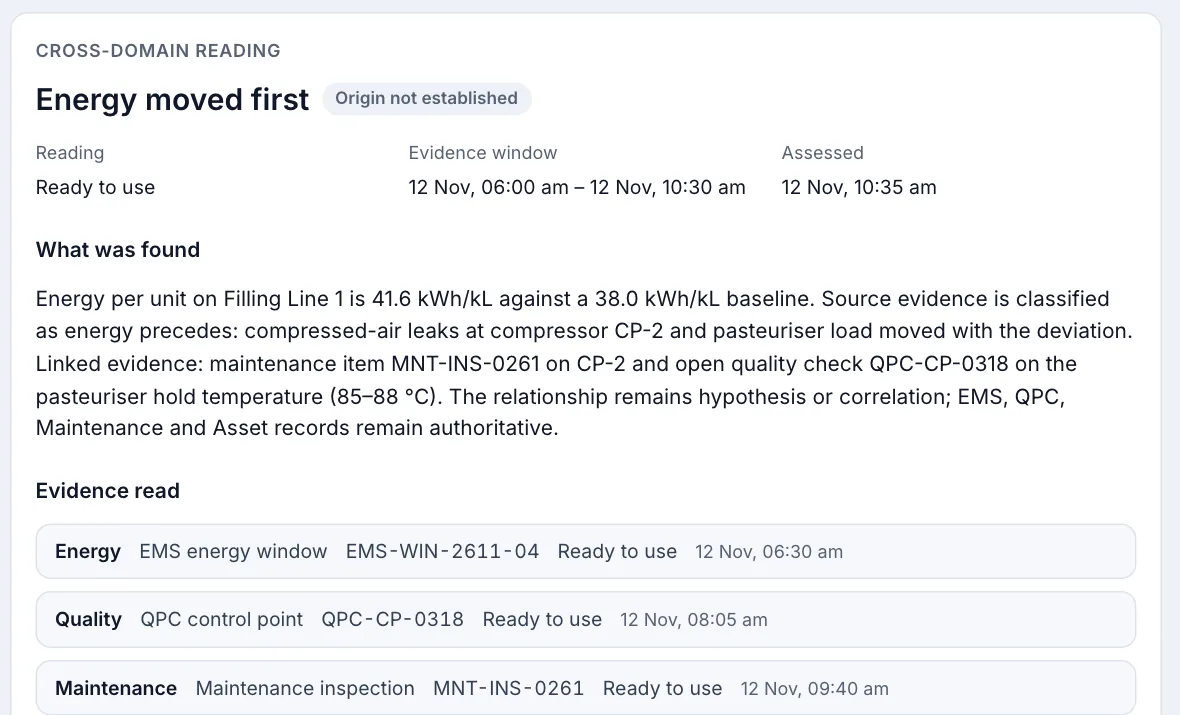
  • Tracks energy and energy per unit against baseline
  • Detects abnormal load and idle running
  • Links energy drift to process, quality and maintenance evidence
  • Counts savings only from verified periods; second-role approval
Example: 41.6 kWh/kL against a 38.0 baseline, linked to compressed-air leaks
Evidence and its strength shownDecides: Energy EngineerNo direct plant change

Shop-floor app

Shared tablets with personal PIN sign-in for operators, chemists, technicians and store keepers. Capture at the point of work, online or offline.

Intelligent alerts

Escalation ladders by role and SLA, with email alerts, so nothing important waits in a chat group.

Reports and exports

Numbered, QR-linked documents and standard reports generated from the plant's own records.

Next step

See PerformIQ on your own plant

Book a no-cost Plant Intelligence Assessment. In about two weeks you get a map of your plant's signals and decision gaps, a value estimate built on your own baseline, and a scoped 90-day pilot plan.